
Advanced mechanical systems have revolutionized how delicate food liquids move through automated processing lines toward global distribution channels. Precision filling technology protects vulnerable aromatic oils from oxygen exposure during high-speed bottling runs, preserving complex flavor profiles for retail consumers.
Large-scale culinary distributors sourcing through sesame oil wholesale channels require strict mechanical standards to avoid oxidation and container leakage across long transit routes. International trading partners like JOLION Foods connect modern automated processing facilities with global commercial markets to meet rigorous packaging requirements.
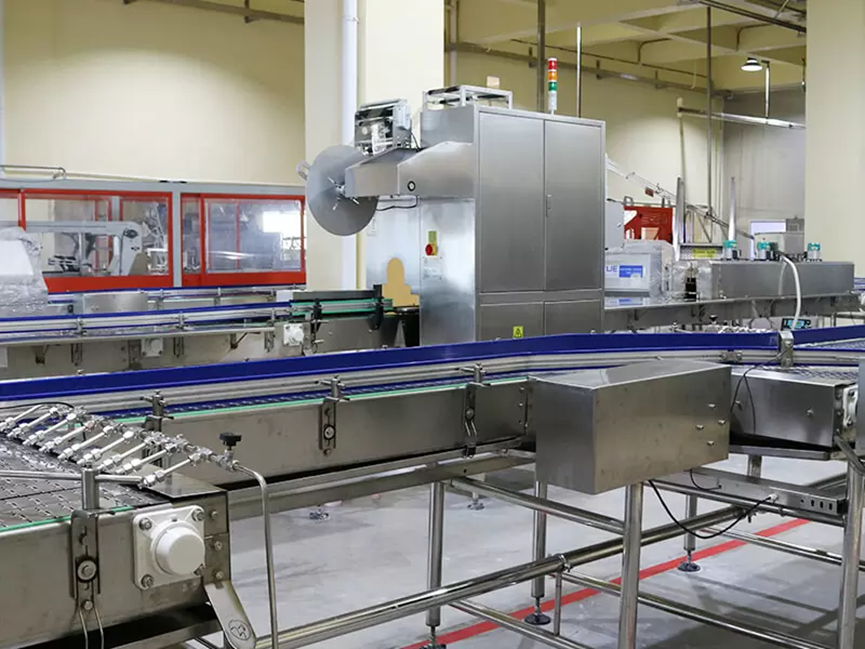
Precision Dosing Mechanics in Liquid Filling Systems
Modern volumetric filling systems utilize high-precision piston pumps and flow meters to dispense exact fluid quantities into waiting containers. Eliminating volume variances across thousands of bottles minimizes product waste while adhering to international net-weight regulations. Dynamic sensors detect bottle placement in milliseconds, preventing accidental spillage on conveyor lines.
Automated liquid lines incorporate controlled nitrogen flushing prior to sealing, with the displacement of ambient air naturally extending shelf life. Minimizing headspace oxygen prevents sensitive fatty acid chains from initiating thermal or oxidative breakdown inside sealed containers. Precision nozzle design prevents drip formation on bottle rims, ensuring clean surfaces during labeling.
Facilities handling large-scale commercial orders through sesame oil wholesale operations depend on automated volume accuracy to maintain consistent product specifications. Advanced sensor networks track fluid movement continuously to detect immediate flow pressure drops. Reliable mechanical engineering guarantees that every retail unit meets identical weight and volume standards.
Atmospheric Isolation and Oxygen Control Technologies
Controlling ambient humidity and temperature within filling chambers protects vulnerable seed extracts from environmental contamination. Enclosed cleanroom environments utilize positive air pressure systems to exclude dust particles and airborne microbes during the exposure window. Strict environmental filtration prevents external impurities from contacting liquid surfaces during bottling.
Modern capping mechanisms apply consistent rotational torque to create hermetic seals that withstand atmospheric pressure changes during air or ocean transport. Synthetic liners inside caps prevent volatile aromatic compounds from escaping through microscopic gaps over extended storage periods. Automated vision systems inspect cap placement instantly to reject improperly sealed bottles automatically.
Distributors procuring inventory via sesame oil wholesale channels benefit from advanced sealing technologies that prevent oxidation during extended transit. Airtight packaging retains delicate top notes from factory production lines directly to kitchen pantries. Protective environmental controls provide international buyers with consistent ingredient quality.
Automated Packaging Integration in Modern Processing
Incorporating a Full-Automatic Packing Machine within processing facilities optimizes workflow by integrating bottle washing, volumetric filling, capping, and labeling into a single continuous sequence. High-speed robotics handle delicate glass and plastic containers gently, minimizing mechanical friction and breakage risks during high-volume operations. This automated integration preserves liquid purity by eliminating manual handling throughout the final packaging phase.
Automated labeling units apply multi-language compliance labels smoothly using heat-resistant adhesives that withstand humid shipping conditions. Secondary packaging systems group finished bottles into corrugated cartons automatically, applying protective dividers to absorb shock during transit. Automated palletizing units stack cartons precisely to maximize container load density for export shipments.
Global supply networks managed by JOLION Foods rely on fully automated packing systems to maintain high throughput and flawless packaging standards for international distribution. Streamlined mechanical operations reduce turn-around times, allowing fresh inventory to ship out quickly to overseas destinations. Modern factory automation supports consistent product presentation across diverse global retail shelves.
Structural Material Considerations for Storage Stability
Selecting appropriate container materials represents a crucial decision in preserving liquid lipids against ambient light degradation. Dark amber or green glass filters harmful ultraviolet wavelengths that catalyze free radical formation in unrefined plant oils. High-density polyethylene provides a durable, lightweight alternative for commercial food service containers.
Interactions between liquid lipids and container walls require careful chemical compatibility testing prior to mass production. Non-reactive glass surfaces ensure that delicate flavor compounds remain unaltered over long storage durations. Specialized inner coatings on metal containers prevent corrosion from trace organic acids present in natural oils.
Procuring certified inventory via a reputable sesame oil wholesale network guarantees that container materials conform to international food-contact standards. Proper material selection prevents flavor contamination and extends pantry shelf life significantly. Careful packaging design ensures that end consumers enjoy fresh, authentic flavors.
Global Supply Standards and Quality Assurance
International food safety protocols govern automated packaging operations to protect public health across global supply chains. Systematic Hazard Analysis Critical Control Point evaluations monitor potential contamination risks at every stage of automated bottling. Continuous thermal and microbiological testing verifies product purity before batches leave processing facilities.
Third-party auditing agencies conduct unannounced facility inspections to verify compliance with international hygiene standards. Digital lot coding printed on bottle necks allows precise traceability from raw seed farm origin to final retail display. Transparent supply documentation simplifies customs clearance procedures across international borders.
Sourcing verified food items through established international partners such as JOLION Foods assures commercial buyers of strict adherence to international safety guidelines. Standardized quality assurance framework builds long-term commercial trust across global distribution networks. Continuous monitoring ensures that every shipment meets strict culinary and health standards.
Conclusion
Understanding the engineering principles, oxygen controls, and material sciences involved in modern liquid packaging helps commercial buyers appreciate the value of automated processing. Advanced mechanical systems protect delicate seed lipids from environmental degradation, ensuring long-term flavor stability and safety.
Partnering with established international supply organizations like JOLION Foods provides food businesses worldwide with access to reliably packaged, high-grade culinary ingredients that meet modern regulatory standards.
